Choosing a manufacturing supplier in 2026 requires more than comparing prices and polished presentations. This guide explains how to evaluate a manufacturing supplier through evidence, not promises. The process begins with capability. Can the supplier produce your part within tolerance, at the required volume, and under realistic delivery conditions? Request recent inspection reports, sample parts, process-flow diagrams, and corrective-action records. Look closely.
A factory tour can reveal details that spreadsheets hide. Watch how operators identify materials, control revisions, and respond to defects. Check whether calibration labels are current. Ask who owns quality when production falls behind. Peter Drucker stated, “Quality in a service or product is not what you put into it. It is what the customer gets out of it.” That principle still matters. Your evaluation should connect supplier processes with customer outcomes, including consistency, traceability, service, and recovery speed.
The 2026 assessment also needs broader questions. Review cybersecurity controls, digital traceability, workforce training, financial stability, and geographic resilience. Verify environmental and labor claims through credible records, not attractive brochures. Test communication before signing a contract. Send a technical question and measure the response time and precision. Small signals matter.
No evaluation is perfect. A successful audit may reflect one unusually prepared day. A low quote may conceal tooling delays, weak documentation, or costly rework. Even a polished dashboard can lie. That is why a staged qualification, pilot order, and measurable supplier scorecard are safer than confidence alone. This introduction sets the foundation for a practical, evidence-based decision.
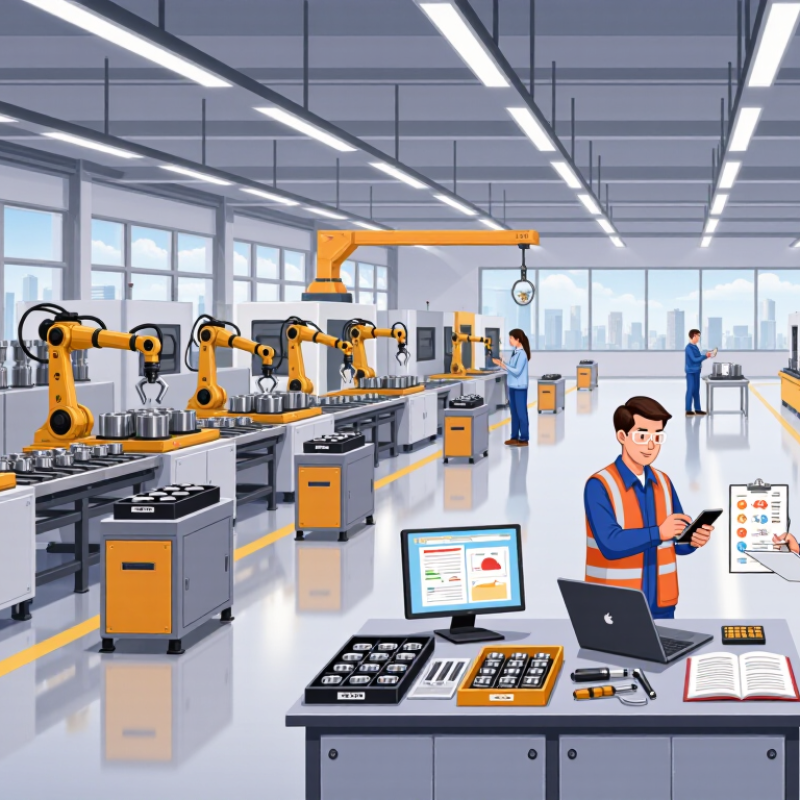
A strong supplier evaluation begins with a precise manufacturing brief. Define the product’s function, materials, dimensions, tolerances, annual volume, target cost, and delivery window. Include drawings, sample photos, packaging details, and acceptable defect limits. Vague requirements create vague quotations. They also hide expensive assumptions.
Separate essential criteria from preferred features. Essential criteria may include process capability, quality certifications, traceability, production capacity, and export experience. Preferred features might include automated inspection or local inventory. A 2023 global supply-chain leader survey reported that 90% of respondents had invested in digital supply-chain tools since 2020. Therefore, ask suppliers how they record production data, approve changes, and share inspection results. A spreadsheet is not always enough.
Score suppliers against weighted criteria, rather than choosing the lowest price. For example, assign quality 30%, delivery reliability 25%, technical capability 20%, total cost 15%, and communication 10%. Request evidence, not promises: recent inspection records, process-flow charts, capacity calculations, and customer-reference details with sensitive information removed. The 2024 Reshoring Initiative data report recorded more than 220,000 announced U.S. manufacturing jobs returning or newly created since 2010, highlighting the growing importance of regional capacity and workforce stability. Still, a polished factory tour can mislead. One supplier may perform well during an audit but struggle with overtime demand. Test this by running a controlled pilot order, measuring defect rates, response times, packaging damage, and actual lead time. I would also repeat the evaluation after three months. Requirements change. Sometimes the original score was simply wrong.
| Evaluation Dimension | Manufacturing Requirement and Verification Evidence | Weight | Supplier A Score / Evidence |
Supplier B Score / Evidence |
Supplier C Score / Evidence |
Supplier D Score / Evidence |
|---|---|---|---|---|---|---|
| Technical Capability | Required process capability, material range, equipment suitability, tolerance control, and documented first-article approval. | 15% | 4.5 / 5Validated process; tolerance capability demonstrated | 3.8 / 5Most processes available; one tolerance gap | 4.2 / 5Strong equipment fit; sample approval pending | 3.1 / 5Limited capability for complex features |
| Quality Management | Current quality-management certification, inspection plan, calibration records, corrective-action process, and traceability by lot. | 15% | 4.6 / 5Complete records and closed corrective actions | 4.1 / 5Documented system; minor audit observations | 3.7 / 5Basic system; traceability improvement needed | 4.3 / 5Strong inspection controls and records |
| Defect Performance | Target outgoing defect rate below 1.0%, with clear measurement method, sampling plan, and evidence from comparable production. | 12% | 4.4 / 50.6% reported defect rate | 3.6 / 51.2% reported defect rate | 4.0 / 50.9% reported defect rate | 4.2 / 50.7% reported defect rate |
| Capacity and Scalability | Available monthly capacity, peak-volume flexibility, labor coverage, equipment utilization, and realistic ramp-up plan. | 12% | 4.0 / 518,000 units/month; 25% headroom | 4.5 / 530,000 units/month; 35% headroom | 3.4 / 512,000 units/month; limited peak capacity | 3.8 / 520,000 units/month; second shift available |
| Delivery Reliability | On-time-in-full delivery target of at least 95%, production planning discipline, lead-time consistency, and escalation procedure. | 12% | 4.3 / 597% on-time delivery over the last 12 months | 3.9 / 594% on-time delivery over the last 12 months | 4.6 / 598% on-time delivery over the last 12 months | 3.5 / 591% on-time delivery over the last 12 months |
| Total Cost of Ownership | Compare unit price, tooling, inspection, packaging, freight, duties, payment terms, warranty exposure, and expected cost changes. | 10% | 4.1 / 5Balanced price and logistics cost | 4.6 / 5Lowest quoted landed cost | 3.8 / 5Higher labor cost; low freight exposure | 4.0 / 5Competitive price; higher tooling charge |
| Financial Resilience | Review financial statements, payment behavior, insurance coverage, customer concentration, and continuity funding. | 8% | 4.2 / 5Stable cash flow and diversified customer base | 3.5 / 5Moderate leverage and customer concentration | 4.0 / 5Stable operations; limited public data | 3.2 / 5Weak liquidity indicators require mitigation |
| Supply Chain Resilience | Approved alternate sources, safety-stock policy, sub-tier visibility, business-continuity plan, and recovery-time objective. | 8% | 4.4 / 5Dual sourcing for critical materials | 3.2 / 5Single source for two critical inputs | 3.9 / 5Contingency plan documented but untested | 3.6 / 5Basic continuity plan; limited sub-tier visibility |
| Sustainability and Compliance | Environmental permits, restricted-substance controls, energy and waste data, labor standards, and compliance documentation. | 5% | 4.3 / 5Verified environmental and labor records | 3.7 / 5Required permits available; emissions data incomplete | 4.1 / 5Good waste controls and material declarations | 3.4 / 5Documentation gaps require corrective action |
| Engineering Collaboration | Design-for-manufacturing support, response time, change-control discipline, prototype support, and technical communication. | 3% | 4.5 / 5Average technical response within 1 business day | 3.8 / 5Average technical response within 2 business days | 4.2 / 5Strong prototype and tooling support | 3.3 / 5Inconsistent engineering response time |
| Weighted Evaluation Result | 4.30 / 5 Preferred |
3.89 / 5 Conditional |
4.02 / 5 Preferred |
3.54 / 5 High Risk |
||
Review quality systems, process records, defect trends, calibration logs, and corrective-action history. Certification helps, but it cannot prove stable performance.
Verify material traceability, worker-safety controls, environmental permits, and subcontractor oversight. Compare production records with the approved process. Do not rely on signed declarations alone.
Request three months of quality data, not selected examples. Check defect rates, overdue actions, inspection results, and evidence that corrections remained effective.
Measure from approved drawing to packed shipment. Compare average and worst-case cycle times across six months. Include engineering changes, rework, and volume increases.
Request a landed-cost worksheet. Include tooling, inspection, packaging, transport, customs-related charges, rework, and possible delays. Cheap capacity can become costly.
Examine machine capability studies, digital traceability, inspection frequency, and backup equipment. Advanced software cannot repair weak supervision. That assumption is easy to miss.
Map critical materials, secondary processors, transport routes, and recovery options. Check inventory policies, supplier concentration, and communication during delays. One missing part can stop production.
Test samples from at least three production lots when possible. Measure dimensions, strength, appearance, and packaging performance against written specifications. Record equipment and test conditions.
Set scorecard weights before reviewing prices. Combine audit results, test data, corrective-action speed, total cost, and delivery history. My scoring can still be wrong.
Re-audit after major equipment, material, or management changes. Also review performance after seasonal overtime. Audits capture one period, not every operating condition.
Learning how to evaluate a manufacturing supplier in 2026 requires a structured review of both operational capabilities and long-term reliability. Begin by defining your product specifications, quality standards, order volumes, target costs, delivery expectations, and communication requirements. Then assess whether each supplier has the necessary equipment, technical expertise, production capacity, certifications, and experience to meet those needs consistently. A strong supplier should also demonstrate effective quality management, regulatory compliance, traceability, cybersecurity awareness, and practical risk-control procedures.
Next, compare total costs rather than focusing only on unit prices. Consider lead times, tooling, logistics, payment terms, technology adoption, flexibility, and supply chain resilience. To determine how to evaluate a manufacturing supplier in practice, conduct a documented facility audit, review relevant records, test samples, and verify production processes before making a final decision. Select the supplier that offers the best balance of quality, transparency, capacity, responsiveness, cost efficiency, and sustainable performance, supported by clear agreements and regular performance reviews.
 HYDRA CNC