How to Improve Surface Finish in Metal Parts in 2026?

Time:2026-10-11 Author:Mason
0%

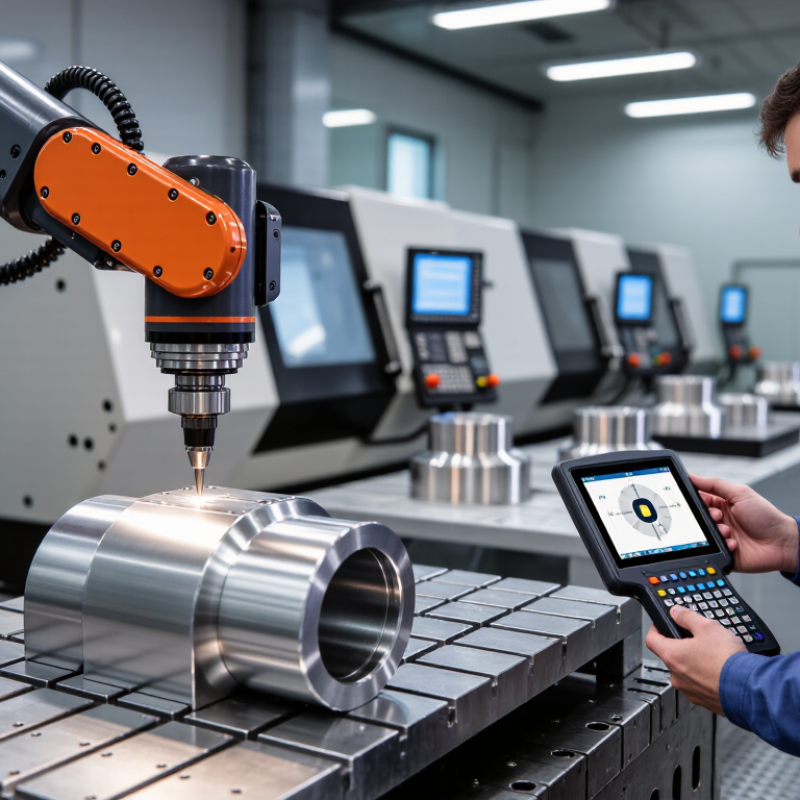
In 2026, manufacturers are asking a practical question: how to improve surface finish in metal parts without slowing production. The answer rarely comes from one machine setting. It comes from controlling the entire process, from material selection to final inspection.

On a CNC shop floor, a sharp tool may leave clean lines on aluminum. The same tool can create chatter on stainless steel. Tool wear, cutting speed, coolant flow, vibration, and workholding all leave visible evidence. A profilometer may show a low Ra value, yet the part can still contain burrs, torn edges, or directional marks. Surface texture is not only a number.

Quality expert W. Edwards Deming said, “Quality comes not from inspection, but from the improvement of the production process.” That principle remains useful for modern metal finishing. Inspectors can identify defects, but stable results require controlled inputs and repeatable methods. In practice, this means testing cutting parameters, checking inserts regularly, and recording surface readings across different batches.

There is no universal recipe. Some recommendations fail when the alloy, geometry, or machine changes. That is worth admitting. Experienced teams combine supplier data, operator judgment, and measurable evidence. They may use grinding, polishing, blasting, tumbling, or chemical finishing, depending on the required function.

The goal is not merely a shinier part. It may involve better sealing, lower friction, improved fatigue performance, or stronger corrosion resistance. This guide examines practical methods, common mistakes, inspection tools, and process decisions that can improve metal surface finish in 2026.
How to Improve Surface Finish in Metal Parts in 2026?

Defining Surface Finish Requirements for Metal Parts

How to Improve Surface Finish in Metal Parts in 2026?

Defining Surface Finish Requirements for Metal Parts

Surface finish requirements should begin with function, not appearance. A smooth surface may reduce friction, support sealing, or improve coating adhesion. It can also increase machining time and cost. Define the working area clearly. A bearing seat, threaded hole, and visible panel may need different requirements.

Use measurable values on the engineering drawing. Ra is common, but it does not describe every surface feature. Rz, lay direction, waviness, and edge condition may also affect performance. For example, a sealing face might need a controlled Ra range and a specified lay direction. A decorative panel may need uniform texture instead. Avoid vague terms such as “smooth” or “high quality.”

Inspection methods must match the requirement. A contact profilometer can measure roughness, while optical systems help review larger areas. Confirm measurement direction, cutoff length, sampling locations, and calibration status. Small details matter. Surface readings can change near edges, holes, or curved sections. Coating thickness and cleaning processes can change the final result, too.

Requirements should remain realistic. Overly tight tolerances sometimes add cost without improving service life. That assumption deserves review. Check the part’s material, machining process, operating load, and cleanliness needs before selecting a target. Build a sample part, inspect it under production conditions, and compare performance rather than relying only on visual judgment. A specification that cannot be measured consistently is not a useful specification.

How to Improve Surface Finish in Metal Parts in 2026?

Defining the required arithmetic average roughness (Ra) before production helps align material selection, machining parameters, inspection methods, and post-processing. The chart shows representative Ra ranges commonly associated with major metalworking processes. Lower Ra values indicate a smoother surface.

Values are typical engineering ranges in micrometres (µm); actual results depend on material, tooling, machine condition, geometry, and process parameters.

Selecting the Right Metal, Tool, and Machining Process

How to Improve Surface Finish in Metal Parts in 2026?

Selecting the Right Metal, Tool, and Machining Process

Surface finish starts with metal selection, not the final polishing step. Aluminum, stainless steel, and hardened tool steel respond differently under identical cutting conditions. A machinist should check hardness, grain structure, and thermal behavior before programming the toolpath. Softer alloys may smear. Hardened materials may chip cutting edges quickly.

Tool geometry also matters. Use a sharp, rigid tool with suitable clearance for the selected metal. A smaller nose radius can reduce cutting pressure, but it may leave visible feed marks. Larger radii often improve finish, although excessive pressure can cause vibration. Match cutting speed, feed rate, and depth of cut through controlled trials. One setting rarely works perfectly.

Tips: Keep the tool overhang short. Measure runout before machining. Apply stable coolant flow. Inspect the surface under angled light, not only by touch. Record every adjustment.

In practice, finishing passes should remove a consistent amount of material. Uneven stock can force the tool to rub, creating heat and dull streaks. Climb milling often produces a cleaner result on rigid equipment. Yet machine rigidity, workholding, and operator experience can change that outcome. I have seen a slower feed improve one part and worsen another. That result needed investigation, not assumption. Surface roughness testing provides stronger evidence than visual judgment alone. Automated finishing may help in 2026, but skilled review remains necessary when tolerances are tight.

How to Improve Surface Finish in Metal Parts in 2026? - Selecting the Right Metal, Tool, and Machining Process

Typical values for properly maintained CNC equipment and stable cutting conditions. Actual results depend on geometry, rigidity, coolant, tool condition, and inspection method.
Material Typical Hardness Recommended Cutting Tool Tool Geometry / Coating Preferred Machining Process Typical Achievable Surface Finish, Ra Practical Finish-Improvement Guidance
Aluminum 6061-T6 ≈95 HB Polished carbide or PCD Sharp positive rake, high helix, polished flute; non-stick edge preparation High-speed finish milling or turning 0.4–1.6 µm with optimized finishing; 1.6–3.2 µm for general machining Use sharp tools, adequate chip evacuation, minimal radial engagement, and avoid built-up edge.
Aluminum 7075-T6 ≈150 HB Fine-grain carbide or PCD Sharp polished cutting edge, high helix, positive rake High-speed contour milling or precision turning 0.4–1.6 µm with a dedicated finish pass Maintain consistent chip load and use a light radial finish pass to reduce tool marks.
Low-Carbon Steel ≈120–180 HB Coated carbide Moderate positive rake, strong edge, wear-resistant coating Finish milling, turning, or cylindrical grinding 0.8–3.2 µm by turning or milling; 0.2–0.8 µm by grinding Control vibration, use a rigid setup, and select feed per revolution according to the required Ra.
Stainless Steel 304 ≈150–220 HB Tough carbide or ceramic for selected high-speed applications Sharp but supported edge, positive rake, heat-resistant coating Stable finish turning, milling, or grinding 0.8–3.2 µm under stable conditions; 0.4–1.6 µm after grinding Avoid dwelling and rubbing, maintain sufficient feed, and apply coolant consistently to limit work hardening.
Stainless Steel 316 ≈150–220 HB Tough, sharp carbide Positive rake, reinforced edge, heat-resistant coating Low-vibration finish turning or grinding 1.6–3.2 µm by machining; 0.2–0.8 µm by grinding or honing Use a rigid workholding arrangement and prevent repeated passes over the same surface without cutting.
Brass ≈80–150 HB Uncoated carbide or polished carbide Sharp edge, moderate rake, polished flutes High-speed turning or milling 0.4–1.6 µm Use sharp tools and firm clamping; excessive clearance or tool runout can produce chatter marks.
Titanium Alloy ≈300–380 HB Sharp carbide with a tough substrate Positive rake, strong edge, heat-resistant coating; avoid excessive edge honing Constant-engagement milling or controlled turning 0.8–3.2 µm; grinding may reach approximately 0.2–0.8 µm Use high-pressure coolant where available, avoid tool rubbing, and maintain a constant cutter engagement.
Hardened Tool Steel, 50–60 HRC ≈480–700 HB Fine-grain carbide, ceramic, or CBN Short overhang, rigid edge, geometry selected for hardness and interruption Hard milling followed by grinding or polishing 0.4–1.6 µm by hard milling; 0.1–0.4 µm by grinding Prioritize machine rigidity, minimize runout, and use a fine finishing step for tight form and finish requirements.
Surface-Finish Selection Guide: Rough machining commonly produces Ra 3.2–12.5 µm, finish milling or turning typically produces Ra 0.8–3.2 µm, grinding commonly produces Ra 0.1–0.8 µm, and honing or polishing can achieve approximately Ra 0.05–0.4 µm when geometry, material, and process control are suitable.

Optimizing Cutting Parameters for a Smoother Surface

How to Improve Surface Finish in Metal Parts in 2026?

Optimizing cutting parameters begins with measurement, not guesswork. ISO 4287 defines Ra as the arithmetic mean roughness value, while ASME B46.1 specifies how surface texture should be evaluated. Use the same cutoff length and measuring direction each time. Otherwise, the numbers may look better than the actual surface.

Published machining trials in CIRP journals from 2022 to 2024 commonly reported that feed rate strongly affects surface roughness. Reducing feed by 20–30% often lowered Ra by roughly 15–35% in turning and milling tests. Start with stability. Keep cutting speed within the tool manufacturer’s tested range, then adjust feed per tooth in small steps. Excessive speed can create heat, built-up edges, or thermal damage. A modest increase in cutting speed sometimes improves finish, but only when chip evacuation remains controlled.

Tool geometry matters too. A larger nose radius can reduce visible feed marks, yet it may increase cutting force and vibration. Keep radial engagement low during finishing passes, and avoid a heavy final cut. The 2023 U.S. Department of Energy manufacturing assessment links compressed-air and coolant waste with inefficient process control, so coolant delivery should be targeted rather than excessive. Measure Ra after each parameter change. A clean formula is tempting, but every machine behaves differently. Even a rigid setup can fail when the workholding is slightly loose.

Applying Secondary Finishing Methods and Surface Treatments

How to Improve Surface Finish in Metal Parts in 2026?

Applying Secondary Finishing Methods and Surface Treatments

Secondary finishing can change a functional metal part into a reliable, service-ready component. Industry market analyses published in 2024 estimate the global metal finishing market at approximately US$110 billion. That scale reflects strong demand for corrosion resistance, wear control, and improved appearance. The U.S. Environmental Protection Agency’s Metal Finishing Sector Notebook identifies more than 20 common finishing operations. These include plating, anodizing, polishing, conversion coating, and cleaning.

The correct method depends on the substrate, service environment, and required surface profile. Anodizing can protect aluminum parts, while electroless nickel improves hardness and uniform coverage. Powder coating suits many external components, but sharp edges may receive thinner coverage. Small details matter. Remove burrs before coating. Clean fingerprints and cutting fluids thoroughly. Surface texture should be measured against ISO 21920 requirements, not judged by sight alone. A bright finish can still hide poor adhesion.

Testing should reflect real service conditions. ASTM B117 salt-spray testing provides useful comparisons, but it does not perfectly predict outdoor performance. That limitation deserves attention. A 2023 materials engineering review found that pretreatment quality often influences coating life more than coating thickness alone. In practice, I would inspect witness panels, measure roughness at multiple points, and record bath or cure conditions. One missed cleaning step can create blistering weeks later. Designing the finish with the machinist and coating technician usually prevents expensive rework.

Inspecting, Measuring, and Maintaining Surface Quality in 2026

In 2026, surface quality begins with disciplined inspection, not visual confidence. I have seen polished parts fail because operators missed shallow tool marks under bright lighting. Use clean, consistent illumination and rotate each part slowly. Inspect edges, holes, and curved areas closely. These locations often hide scratches, burrs, or uneven finishing.

Measurement should support what the eye cannot confirm. A calibrated roughness tester can record Ra and other suitable values at defined locations. Keep the probe clean, positioned correctly, and aligned with the machining direction when required. Record the part number, measurement site, tool condition, and operator. Small details matter. Our early records lacked location data, making useful comparisons difficult. That mistake delayed corrective action.

Maintenance must connect inspection results with production habits. Check abrasive tools, cutting inserts, coolant condition, fixture contact points, and cleaning methods at regular intervals. Replace worn tools before their marks become obvious. Store finished parts with separators, because metal-on-metal contact can damage a good surface quickly. Recheck samples after process changes, temperature shifts, or extended machine use. One reading is not enough. Trends are more reliable.

A practical quality system should define acceptance criteria, calibration intervals, lighting conditions, and measurement locations. Independent review can reduce personal bias, especially when a finish looks acceptable but measures poorly. Leave room for reflection. A rushed inspection may pass today’s batch and create tomorrow’s complaint.

FAQS

How should surface finish requirements be defined?

Start with the part’s function, not its appearance. A bearing seat may need low friction. A visible panel may need consistent texture. Avoid vague terms like “smooth.”

Which surface measurements should appear on an engineering drawing?

Specify measurable values such as Ra or Rz. Add lay direction, waviness, and edge conditions when performance depends on them. Ra alone may miss important surface features.

Can every area of one metal part use the same finish requirement?

Usually not. Threaded holes, sealing faces, bearing seats, and visible panels often need different targets. Define each working area clearly.

How should surface roughness be inspected?

Match the inspection method to the requirement. A contact instrument suits roughness readings. Optical inspection can review larger areas. Record direction, cutoff length, sampling locations, and calibration status.

Why can roughness readings change across the same part?

Readings may vary near edges, holes, or curved sections. Coatings and cleaning can also change the final surface. Measure representative areas, not only convenient ones.

Does a lower Ra always improve part performance?

No. A smoother surface can reduce friction or support sealing. It can also increase machining time and cost. That assumption deserves review.

How can cutting parameters improve surface finish?

Reduce feed gradually and measure Ra after each change. Trials often show that a 20–30% feed reduction lowers roughness. Cutting speed should remain within a tested range.

What tooling and machine conditions affect surface finish?

A larger nose radius may reduce feed marks, but it can increase vibration. Keep radial engagement low during finishing. Check workholding carefully. A slightly loose setup can ruin an otherwise stable process.

How should coolant and chip removal be managed?

Direct coolant toward the cutting zone. Excessive coolant may waste resources without improving results. Poor chip evacuation can create heat, built-up edges, or surface damage.

What is a practical way to validate a finish specification?

Produce a sample part under normal production conditions. Inspect it and compare actual performance. A specification that cannot be measured consistently is not useful. I would still question every unnecessary tolerance.

Conclusion

Improving the surface finish of metal parts in 2026 requires a structured approach that begins with clearly defining quality requirements. Factors such as roughness, visual appearance, dimensional accuracy, corrosion resistance, and intended use should guide the selection of the metal, cutting tool, and machining process. Material properties and part geometry must be considered together to achieve consistent results without creating unnecessary production costs.

To understand how to improve surface finish in metal parts, manufacturers should optimize cutting speed, feed rate, depth of cut, tool condition, coolant application, and machine stability. Lower vibration and properly maintained equipment can significantly reduce marks and irregularities. When machining alone is not enough, secondary processes such as polishing, grinding, deburring, coating, or controlled surface treatment can provide the required finish. Finally, surface quality should be verified through suitable measuring equipment and documented inspections. Regular monitoring, tool replacement, and process adjustments help maintain reliable results throughout production.
Mason

Mason

Mason is a seasoned marketing professional with a deep expertise in the company's offerings and a passion for driving brand awareness. With a strong background in digital marketing strategies, he has an innate ability to connect with diverse audiences and effectively communicate product benefits.......